Sheet metal enclosure design is not simply a matter of wrapping electronics in bent material. It is a cross-disciplinary exercise in user experience, structural performance, thermal behavior, regulatory needs, assembly strategy, and manufacturing economics. The strongest enclosures look intentional because their underlying engineering decisions were intentional.
For founders and product teams, the goal is not a beautiful CAD rendering. It is an enclosure that protects the product, supports its function, communicates its value, and can be built consistently at the volumes the business needs.
Start With the Product Architecture, Not the Outer Skin
The enclosure should follow a clear product architecture. Before defining seams, bends, and cosmetic surfaces, establish what must live inside: PCB dimensions, battery format, displays, antennas, cable routing, connectors, fans, heat-generating components, mounting points, and serviceable parts. Each element places constraints on the housing, and ignoring those constraints early creates expensive revisions later.
A power supply may need isolation from sensitive signal electronics. A radio module may require a nonmetallic antenna window or carefully planned antenna placement. A medical or scientific device may need a sealed interface, cleanable surfaces, tamper resistance, or access for calibration. Public-facing equipment may need impact resistance and protected cable exits. The enclosure is where these requirements meet.
This is why industrial design and mechanical engineering need to work from the same layout. Industrial design defines how the product should be understood and handled. Mechanical engineering turns that intent into wall clearances, fastener locations, tolerances, grounding paths, and manufacturable geometry. Electronics engineering validates that the board and components can actually inhabit the proposed volume.
Define the environment before choosing the material
Sheet metal is often selected because it is durable, recyclable, readily available, and suitable for a wide range of fabrication processes. But material choice should be driven by the operating environment and product priorities.
Cold-rolled steel can be cost-effective and stiff, particularly for indoor equipment. Stainless steel offers corrosion resistance and can suit hygienic or demanding environments, although it is harder to form and can raise fabrication costs. Aluminum reduces weight, resists corrosion, and dissipates heat effectively, making it attractive for portable products and electronics-heavy systems. Each option also responds differently to finishing, welding, grounding, and cosmetic requirements.
The right answer depends on the product. An indoor control unit and an outdoor digital-signage assembly should not be designed around the same assumptions. Define expected handling, vibration, temperature exposure, moisture, chemical contact, impact risk, and desired service life before locking the material and gauge.
Design Bends, Seams, and Features for the Shop Floor
A fabrication supplier does not manufacture a CAD model. They laser-cut, punch, bend, weld, fasten, finish, and inspect a set of parts within process limits. Good sheet metal enclosure design accounts for those limits from the beginning.
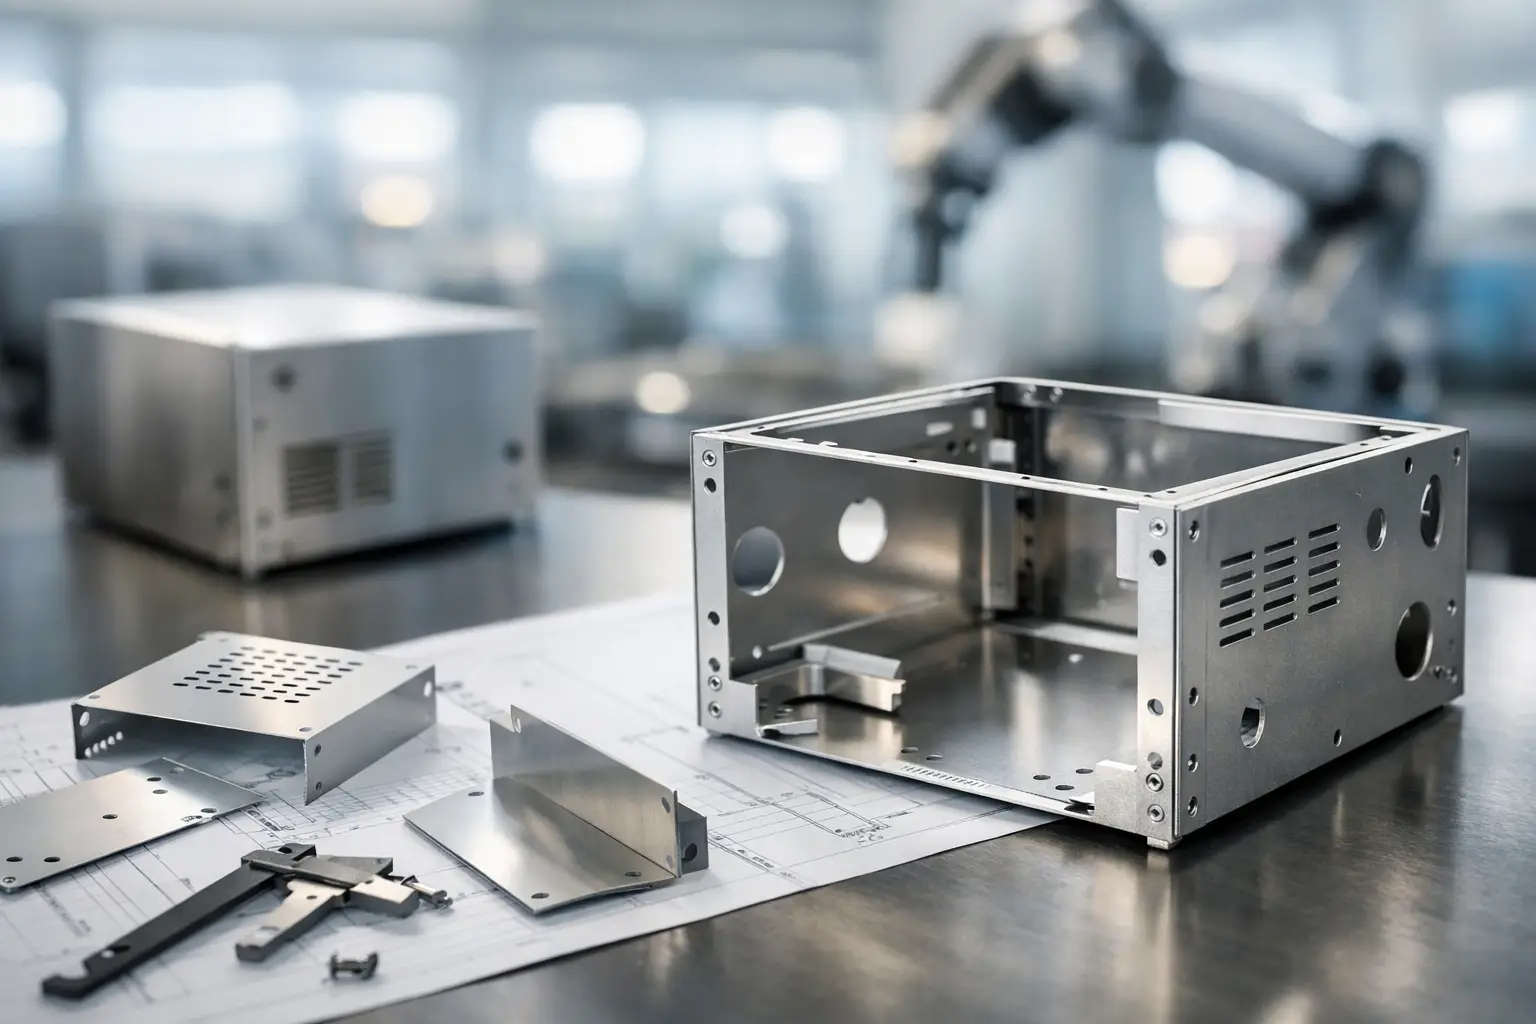
Bend radii, flange lengths, hole placement, and feature spacing all affect whether a part can be formed predictably. A hole placed too close to a bend may distort. A flange that is too short may be difficult to form. A complex geometry may require multiple setups or custom tooling, increasing both cost and lead time. These are not minor details when a program moves from ten prototypes to a production run.
Designers should also avoid treating flat patterns as an afterthought. Bend allowances and bend deductions vary by material, thickness, bend radius, and fabrication method. Experienced suppliers can help establish these values, but the engineering team needs to design with a realistic manufacturing process in mind rather than assuming every bend behaves identically.
Choose a construction strategy early
The way an enclosure comes together influences appearance, serviceability, assembly time, and cost. A folded shell with a removable rear panel can offer quick internal access. A clamshell construction may create a cleaner user-facing form but demands careful seam control. Separate front and rear panels can simplify connector access and allow different finishes, while welded construction can improve stiffness and discourage tampering.
Fasteners are another strategic decision. Standard screws are accessible and service-friendly. Captive screws reduce lost hardware during field maintenance. PEM studs, nuts, and standoffs can create reliable mounting features without loose internal hardware. Spot welding, riveting, and clinching may reduce assembly steps in higher-volume programs, but they can complicate repair or disassembly.
There is no universal best construction. A device expected to be repaired in the field needs a different approach than a sealed commercial product assembled once at the factory. Make that decision based on the complete product lifecycle, not only the first assembly operation.
Treat Electronics Integration as a First-Class Requirement
Metal enclosures offer excellent physical protection and can provide useful electromagnetic shielding. They also create challenges that cannot be solved with late-stage cutouts.
Connector locations should be based on insertion force, plug clearance, cable bend radius, user reach, and strain relief. A connector that technically fits through a panel may still be frustrating to use if adjacent ports interfere with each other or a thick cable cannot route naturally. Controls, displays, indicators, and labels deserve the same scrutiny. Their placement should support fast comprehension, especially for products used in industrial, transit, laboratory, or outdoor settings.
Thermal management needs equal attention. Metal can spread heat effectively, but it is not automatically a cooling solution. Determine how heat moves from components to the enclosure, whether venting is permissible, where airflow enters and exits, and how dust or water protection will affect the system. Adding louvers late can weaken a panel, compromise ingress protection, or create an unwanted path for electromagnetic emissions.
Grounding is also a mechanical design issue. Paint and powder coating can insulate surfaces that need electrical contact. If chassis grounding is required, specify controlled bare-metal contact points, grounding hardware, and assembly instructions. Small details like these prevent late failures during compliance testing.
Build for Tolerances, Finishes, and Real Assembly
An enclosure can be dimensionally correct on paper and still fail during assembly because tolerance stack-up was not considered. Multiple bent panels, PEM hardware, gaskets, PCB mounting features, and cosmetic covers all introduce variation. Critical interfaces need intentional clearance, alignment features, and datum strategies.
Use locating tabs, slots, pilot features, and asymmetric patterns where they prevent incorrect assembly. Give technicians enough access to install screws, route harnesses, and connect components without fighting the housing. If a technician needs three hands to close the enclosure, the design needs more work.
Finishing should be specified as part of the design, not selected after prototypes are built. Powder coating is durable and available in many colors and textures, but it adds thickness and can affect tight fits or grounding points. Anodizing suits aluminum and can create a refined finish, but color consistency and scratch visibility should be evaluated. Brushed stainless can communicate durability, while also making fingerprints and grain direction relevant aesthetic considerations.
Prototype parts may hide these issues because they are often fabricated slowly and adjusted by hand. Production reveals them. At SurfaceID, enclosure development is validated through CAD reviews, functional prototypes, assembly trials, and manufacturer feedback so the product team can resolve problems while changes are still manageable.
Reduce Risk With Purposeful Prototype Stages
Not every question requires a fully finished prototype. Early folded-metal samples can validate scale, ergonomics, connector access, and assembly sequence. Representative thermal builds can test heat paths and airflow. Cosmetic samples can confirm color, texture, seam quality, and perceived value. Pilot builds can expose sourcing, packaging, and inspection issues that CAD alone cannot reveal.
The key is to test the decisions with the highest downstream cost. If a design depends on a tight gasket seal, validate it. If the enclosure must survive vibration, drop, or outdoor exposure, build those tests into the development plan. If users must access a control while wearing gloves, test it with actual gloves rather than relying on clearance dimensions.
A supplier conversation is valuable well before a purchase order. Fabricators can flag challenging bends, suggest alternate construction methods, identify standard hardware, and advise where a small geometry change could eliminate an operation. Their input should sharpen the design intent, not replace it.
The enclosure is often the first physical proof that a product belongs in the market. Give it the same strategic attention as the electronics inside it, and it can carry the product from first prototype to repeatable production with far fewer surprises.